

Content last revised on October 11, 2026
M150XN07-V9 Installation and Compatibility Checks
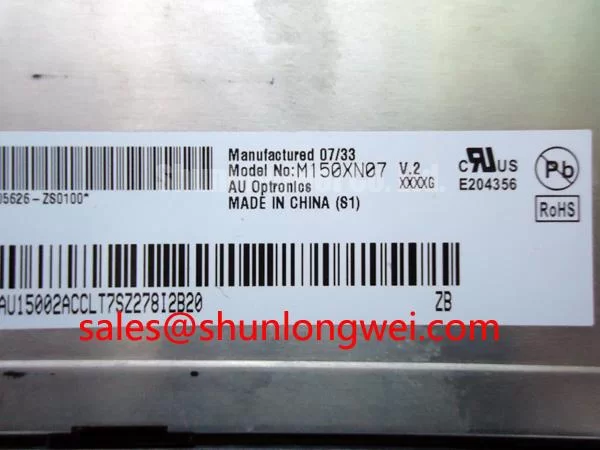
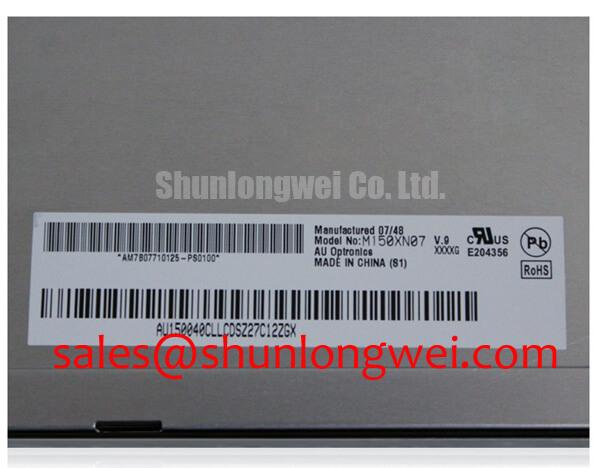
- Confirm the installed panel marking against M150XN07-V9 before removing the original display.
- Record the existing connector orientation, cable keying, and controller board configuration.
- Check the open-frame bezel clearance and gasket contact area for uneven pressure or distortion.
- Isolate the display supply and backlight circuitry before disconnecting the panel cable.
M150XN07-V9 is identified in the supplied information as an Innolux / AUO industrial-grade LCD and HMI panel in a TFT-LCD active-matrix color display module format. The supplied product classification is Decoded Baseline / Standard Form Factor. This makes mechanical envelope, controller compatibility, signal mapping, and backlight architecture the first practical checks when evaluating it for an equipment repair or replacement project.
| Product model | M150XN07-V9 |
| Manufacturer reference | Innolux / AUO |
| Product category | Industrial Grade LCD/HMI Panel |
| Module construction | TFT-LCD Active Matrix Color Display Module |
| Specification status | Decoded Baseline / Standard Form Factor |
| Application evaluation | Industrial HMI, operator console, monitoring panel, and SCADA display replacement assessment |
The supplied baseline does not establish a confirmed native resolution, active-area dimension, connector pinout, logic supply, backlight type, or optical performance value. These characteristics should be matched against the original panel documentation and the host controller before procurement approval. The Innolux Corporation Global Industrial Display Portfolio is a useful manufacturer-level reference for understanding the company’s industrial display range, while the individual replacement decision remains dependent on the installed system interface.
Flush-Mount Open-Frame Bezel Integration and Perimeter Gasket Shock Isolation
Start mechanical integration by placing the replacement panel in the existing bezel without tightening the fasteners, then inspect the perimeter contact line from all four sides. A flush-mounted industrial display needs even support around the frame rather than concentrated loading at isolated corners. Uneven bezel pressure can produce localized optical non-uniformity, visible dark areas, or intermittent changes when the enclosure is exposed to vibration.
The standard form factor classification is useful for initial mechanical screening, but it should not be treated as confirmation that the panel is a direct drop-in replacement for every 15-inch-class enclosure. Compare the original cutout, mounting-hole pattern, connector access, panel depth, and rear clearance. The enclosure should provide stable support without allowing the glass or frame to become a structural load-bearing member.
For a cross-pattern installation using M3 hardware, 0.35 to 0.45 N·m is a general design consideration for controlled fastening, not an Innolux / AUO factory specification for this model. The final assembly method should follow the enclosure manufacturer’s mechanical drawing and the original equipment service procedure. Tighten progressively across the pattern, checking that the bezel remains planar after each adjustment. A gasket should isolate small enclosure irregularities while avoiding compression that transfers a point load into the display perimeter.
When a panel shows a dark-field patch after installation, release the bezel pressure and compare the image before and after re-seating. If the artifact changes with the mounting condition, inspect gasket overlap, screw alignment, frame contact, and cable routing before replacing the panel. This approach separates an optical or mechanical assembly issue from a display-cell or controller fault without assigning a single cause prematurely.
Cold environments require additional attention to response behavior. Liquid-crystal response can become slower as ambient temperature falls, which may appear as extended grey-to-grey transitions, motion smear, or delayed image settling. This is an application-level design consideration rather than a confirmed operating-temperature specification for M150XN07-V9. If the host equipment operates in a sub-zero enclosure, the system designer should validate warm-up behavior, condensation control, image refresh requirements, and any enclosure heating method as a complete system.
For a high-voltage substation protection or SCADA dispatch console, the panel should also be checked against the console’s viewing window, service-door movement, and cable bend path. A display that fits the cutout may still be unsuitable if the rear connector interferes with the controller carrier or if the bezel transfers cabinet vibration into the panel frame. For same-size or same-resolution evaluation work, engineers may also compare the mechanical and interface requirements of LQ10D213 without assuming interchangeability.
Logic Supply Voltage Sequencing and Interface Compatibility
Logic power and display data compatibility should be established before the first image test. The supplied product information does not confirm whether the installed version uses a particular logic voltage, LVDS arrangement, TTL interface, JEIDA mapping, or VESA mapping. The system integrator should verify the required supply voltage from the original panel documentation and compare it with the host controller output.
Some industrial display controllers support selectable logic rails, but that capability belongs to the controller design and must not be attributed to M150XN07-V9 without a matching panel datasheet. Apply the original power-up sequence during bench evaluation and observe the relationship between logic supply, display enable, backlight enable, and video activity. If the panel is powered before the controller signal is stable, the resulting behavior may include a blank screen, unstable initialization, or a temporary split image. These symptoms require comparison with a known-good panel and controller combination.
The requested 3.3 V and 5.0 V values should therefore be treated as candidate system rails for compatibility investigation, not as confirmed dual-rated specifications for this model. The same distinction applies to a proposed supply rise-time window. A power-on profile such as 0.5 ms to 10 ms may be used only as a controller-side engineering test condition when supported by the relevant documentation; it is not an official M150XN07-V9 rating in the supplied baseline.
For LVDS implementations, route each differential pair as a controlled transmission path and maintain consistent geometry through the connector, cable, and host board. A nominal 100-ohm differential impedance with approximately 10 percent tolerance is a common interface design consideration, not a published module parameter here. The board designer should use the cable specification and transmitter-receiver requirements to determine the actual target. Pair skew, reference-plane continuity, connector insertion, and return-current paths should be assessed together rather than corrected by changing only one trace.
JEIDA and VESA mapping differences can produce incorrect color order, unusual tonal transitions, or split-screen artifacts even when the panel illuminates normally. Compare the controller’s bit assignment with the original panel configuration and verify the pixel clock, data enable, and synchronization behavior at the receiver. An oscilloscope or logic analyzer can help identify whether the fault follows the controller output, the cable, or the panel input.
When the display is evaluated in a SCADA console, retain the original cable keying and shielding arrangement during the first test. Do not force a connector that has a similar pitch but a different pin assignment. The correct replacement decision depends on electrical mapping as well as physical fit, and a standard form factor does not establish pin-to-pin compatibility.
Radiated Emissions Evaluation and Backplate Grounding
Control of radiated noise begins with the complete display assembly, including the controller, cable, backplate, enclosure, and nearby power electronics. M150XN07-V9 should not be described as independently compliant with CISPR Class A or Class B because EMC performance is determined at equipment level. The display module may be evaluated within a system that is tested against the applicable emissions standard, but the module itself is not an independent EMC certification.
A shielded LVDS or FFC cable should have a deliberate termination strategy at the host and panel ends. The shield path should be short, continuous, and mechanically bonded to the intended chassis reference where the system design requires it. A 360-degree shield connection is a general design consideration for reducing high-frequency discontinuities; it is not a guaranteed feature of every cable supplied with this panel. Confirm the actual cable construction before specifying a replacement.
Pixel jitter and horizontal noise bands near variable-frequency motor drives can result from several interacting conditions, including common-mode coupling, inadequate return paths, cable routing, controller timing, or grounding topology. Compare the display image while the motor drive is disabled and enabled, then monitor the clock and data signals at the panel-side connector. If the disturbance changes with cable position or enclosure bonding, examine the current return path and shield termination before changing the display module.
Common-mode ferrite components may be considered in the system cable path when measurements show a conducted or radiated interference problem. Their impedance profile must match the signal bandwidth and common-mode noise spectrum; adding an unspecified component can also degrade signal quality. This is an engineering recommendation for system tuning, not an internal feature or guaranteed accessory of M150XN07-V9.
Clock jitter and data hold margin should be checked across the intended temperature range and supply conditions. The display vendor’s interface timing limits, the controller transmitter specification, and the cable propagation characteristics must be considered together. A proposed skew budget such as 50 ps may be used as a design target only when it is derived from the actual link timing budget. It should not be presented as a factory limit for this panel.
For an industrial HMI or substation console, route display cables away from switching-node conductors and high-current motor paths where the enclosure layout permits. The backplate should provide a repeatable reference for the display frame and cable shield, while protective-earth and signal-ground relationships remain defined by the system safety architecture. The Industrial Display & HMI Solutions resource provides broader context for enclosure, interface, and environmental integration decisions.
Backlight Architecture and Ignition or Driver Fault Diagnosis
Backlight identification is a required replacement check because the supplied baseline classifies M150XN07-V9 as a TFT-LCD module but does not confirm whether the installed unit uses a CCFL inverter arrangement or an LED backlight input. Do not connect a CCFL high-voltage inverter to an LED interface, or an LED constant-current driver to a CCFL assembly. The original panel label, wiring, controller board, and service documentation must establish the backlight architecture before power is applied.
For a CCFL-based system, cold ignition can create a high-voltage transient and may be accompanied by a short acoustic signature from the inverter. A proposed 1500 to 1650 Vrms ignition range must be treated as an application-specific test reference, not as a confirmed M150XN07-V9 module specification. Use the inverter manufacturer’s measurement procedure and suitable high-voltage equipment. Inspect for open-lamp detection, output imbalance, connector tracking, and insulation clearance when the lamp fails to strike or extinguishes after startup.
For an LED-based system, the correct driver is a regulated constant-current source matched to the panel’s backlight configuration. Open-string and short-string protection belong to the driver architecture, not automatically to the LCD module. During troubleshooting, capture the driver enable signal, current regulation behavior, fault output, and output response during connection and disconnection events. A dark screen with an active image signal may indicate a backlight path issue, but the driver, cable, connector, panel backlight, and control signal should be checked as separate elements.
PWM dimming should be evaluated for visible modulation, camera banding, audible interaction with the driver, and compatibility with the controller’s enable logic. A 200 Hz to 1 kHz range can be a system tuning region for some industrial LED drivers, but it is not a confirmed specification for this model. The designer should select the dimming method and frequency from the driver datasheet, then verify luminance stability and image behavior across the required brightness range.
Claims about a 50,000-hour half-life or MTBF should not be assigned to M150XN07-V9 without an authoritative optical reliability specification defining temperature, drive current, duty cycle, and failure criteria. For field service, record whether the image remains visible under external illumination, whether the backlight enable signal changes, and whether the driver reports an open or short condition. This evidence helps determine whether the replacement decision concerns the LCD module, the backlight assembly, or the host power electronics.
When integrating the panel into a dispatch console, verify the original brightness control method, connector pinout, backlight enable polarity, and enclosure airflow. The final acceptance test should include cold startup, normal operating brightness, dimming transitions, cable movement, and operation alongside the cabinet’s switching equipment. 💡 Pro Tip: Keep high-speed display pairs referenced to a continuous return path and separate them from backlight and power-switching conductors during the first layout review.