



Content last revised on October 1, 2026
Combating Contact Resistance Escalation across Bezel Fingers under Mechanical Vibration
With the equipment isolated, inspect the SX25S004 bezel contact area and measure continuity through the elastomeric zebra strip while gently applying controlled mechanical pressure to the panel assembly. A changing reading or intermittent row and column response should be compared with the known-good signal path before any connector adjustment is attempted.
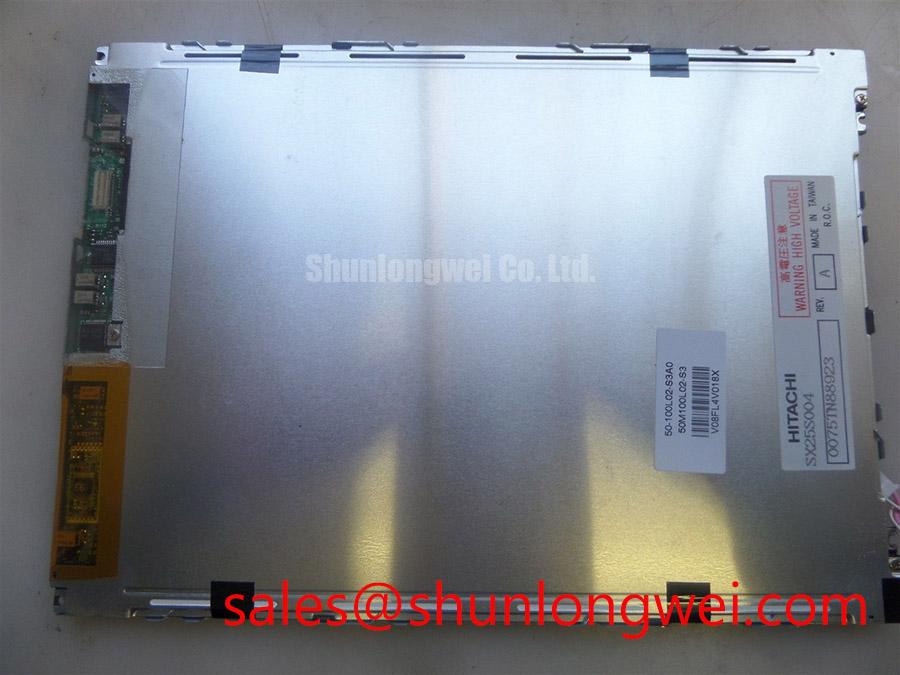
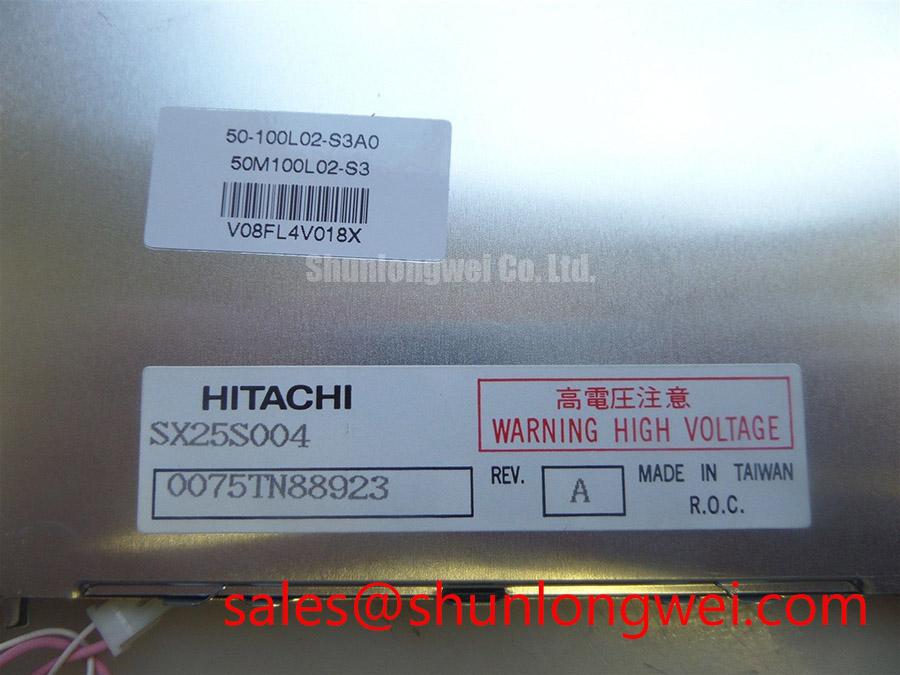
The SX25S004 is identified in the supplied factory information as an FSTN / STN monochrome passive matrix LCD panel. Its passive matrix construction makes the mechanical relationship between the glass panel, zebra connector, bezel fingers, and carrier frame important during service. Oxidation, contamination, uneven compression, or displacement caused by vibration can interrupt selected rows or columns without proving that the LCD glass itself has failed.
Use a clean, controlled inspection method on the contact surfaces. Check whether the bezel applies even pressure along the complete connector width. A localized gap can produce a missing display segment, a partial row, or a column that returns briefly when the chassis is flexed. That symptom should be documented against connector alignment and mechanical condition rather than assigned to one component without measurement.
The clamping method must be treated as a design consideration. The supplied official parameter set does not confirm a model-specific bezel pressure, compression distance, fastening torque, or connector tolerance for SX25S004. The equipment designer should therefore establish the required compression from the original mechanical drawing and validate it across temperature and vibration conditions. Excessive force can stress the glass or create non-uniform optical behavior, while insufficient force can permit contact movement.
For systems using a 4-bit or 8-bit parallel interface, probe the control activity at CP, LP, and FLM against the original controller documentation. A missing row or column combined with stable control timing points toward a possible contact or panel-path issue, but a distorted clock edge or unstable frame signal can create a similar visual symptom. Oscilloscope measurements should be made at the panel connector with the installed cable and grounding arrangement in place.
Power sequencing also requires system-level verification. Confirm that the logic supply reaches its valid operating state before the negative LCD bias rail is enabled, in accordance with the original panel and controller documentation. Do not assign a universal voltage, delay, or bias sequence to SX25S004 from the product category alone. The integrator should verify the required sequence and monitor startup and shutdown behavior during repeated power cycling.
For a same-family sourcing comparison, engineers may review LM64P89 as a separate display option. It should be evaluated by its own documented interface, dimensions, optical characteristics, and electrical requirements rather than treated as an automatic substitute for SX25S004.
Suppressing Ghosting and Crosstalk via Precision Multi-Level Bias Voltage Dividers
Measure the LCD bias rails directly at the panel connector while displaying a stable high-contrast pattern, then compare ripple and settling behavior with a known-good controller and the original panel documentation. Ghosting, contrast drift, and cross-coupled segments should be assessed alongside supply noise, grounding, cable routing, and temperature rather than attributed to the LCD panel alone.
FSTN and STN displays depend on controlled bias conditions for consistent segment contrast. The supplied factory data confirms the display technology but does not provide a verified SX25S004 value for VEE, V0, bias-divider resistance, ripple limit, temperature coefficient, or thermistor curve. Those values must not be inferred from the model name or from another monochrome panel.
A practical diagnostic sequence begins by recording the positive logic rail, the negative bias rail where fitted, and the reference or contrast node during power-up, steady operation, and shutdown. Measure at the panel-side connector because cable resistance, return-current paths, and controller-board impedance can change the voltage seen by the LCD. A rail that appears clean at the power supply may show disturbance at the panel when the display cable and backlight circuitry are active.
Ghosting can also be associated with an unsuitable bias-divider topology, excessive coupling between control lines, or a return path shared with a switching backlight circuit. The design consideration is to keep bias generation quiet and isolate sensitive LCD reference nodes from high-current or high-frequency paths. The final divider values, filtering, and compensation network remain system-determined and require validation with the actual controller and cable assembly.
Temperature testing should include both contrast stability and response behavior. At low temperature, liquid-crystal viscosity can slow optical transitions; at elevated temperature, polarizer and display materials may experience accelerated aging. These are general display design considerations, not SX25S004 field-life guarantees. Record the displayed pattern, ambient and panel temperature, supply conditions, and recovery time so that a service decision is based on repeatable evidence.
Reflective monochrome panels can behave differently under changing ambient illumination. A contrast complaint observed in a bright equipment cabin may involve viewing angle, bezel reflections, cover-lens contamination, or illumination geometry rather than a bias fault. Check the optical stack and enclosure condition before changing the controller voltage. Any modification to the bias network should be tested for segment uniformity and long-duration stability.
When the display is part of a telematics or HMI node, the data network should be diagnosed separately from the LCD interface. Industrial Ethernet technologies such as EtherCAT and PROFINET can deliver system data to a display controller, but network integrity does not confirm correct local LCD biasing. Likewise, refresh-rate terminology used for modern active-matrix displays should not be transferred to this passive-matrix panel without controller-specific evidence; the relevant reference is provided in this display refresh rate overview.
Evaluating High-Voltage CCFL Strike Waveforms and Open-Lamp Trip Thresholds Where Applicable
Disconnect the panel from the high-voltage inverter and identify the installed illumination architecture before measuring any lamp circuit; the supplied SX25S004 factory data confirms an FSTN / STN monochrome LCD panel but does not confirm a CCFL lamp, LED backlight, inverter, ignition waveform, lamp current, or open-lamp threshold.
That distinction is essential during a replacement assessment. A panel model should not be assigned a CCFL or LED interface merely because a particular machine used one illumination arrangement. The system integrator should verify the backlight type, connector pinout, drive requirements, and mechanical lamp arrangement from the original equipment documentation and the installed assembly.
Where a CCFL inverter is confirmed by the equipment documentation, use an appropriately rated high-voltage probe and follow the inverter manufacturer’s isolation procedure. Inspect the lamp leads, insulation, grounding surfaces, and clearance around the panel frame. A strike failure, intermittent illumination, or inverter shutdown can involve the lamp, wiring, inverter protection circuit, connector seating, or enclosure contamination. It cannot be assigned to SX25S004 without separating those conditions through measurement.
Do not apply the numerical ignition voltage, sustained lamp current, ripple limit, or trip threshold from an unrelated display assembly. No such values are included in the supplied official SX25S004 parameter set. The correct engineering method is to compare the installed inverter’s documented operating limits with the original lamp specification, then verify the waveform and protection response under controlled conditions.
For LED-equipped systems, the investigation changes to constant-current regulation, thermal dissipation, dimming behavior, and connector polarity. The model information provided here does not establish an LED current rating or a supported PWM frequency. Any statement about constant-current efficiency, flicker performance, or a 50,000-hour service rating would require an applicable manufacturer document for the complete display or backlight assembly, not a general LCD category description.
In a heavy mining shovel or earthmoving equipment telematics display, vibration and contamination can affect illumination wiring even when the LCD image path remains functional. Check cable retention, strain relief, enclosure sealing, and heat removal as part of the installed assembly. A replacement decision should record whether the fault follows the panel, the inverter or driver, the cable, or the machine-side power and control wiring.
Maintenance Note: Inspect the display enclosure’s cooling path and sealing gasket at scheduled service intervals, because blocked airflow or a displaced gasket can increase thermal stress and permit contamination at the bezel and connector area.
The linked LM64P839 may be reviewed as a separate display-related device when evaluating a compatible system solution, but its electrical and mechanical requirements must be confirmed independently. It should not be treated as an assumed backlight driver for SX25S004.
Data Setup and Hold Time Margin Verification on Flat Ribbon Flex Cables
Probe FLM, LP, and CP at the SX25S004 panel connector with the production flat-ribbon cable installed, and compare setup, hold, edge quality, and return-path behavior with the original controller documentation. A display that becomes unstable when the cable is moved may indicate impedance discontinuity, contact movement, excessive capacitance, grounding weakness, or controller timing stress; the waveform must distinguish these possibilities.
Parallel passive-matrix interfaces are sensitive to cable construction and connector geometry because the panel receives row, column, and timing information through multiple conductors. Cable length, conductor arrangement, shielding, reference returns, and connector contact condition can change edge shape at the panel even when the controller output appears correct at its own board connector.
Use a high-impedance probe with the shortest practical ground connection and avoid loading the signal under test. Capture CP in relation to the data lines, then check LP and FLM during a complete frame. The purpose is to confirm that the panel-side transitions remain clearly separated from the controller’s switching noise. The exact allowable timing values are not included in the supplied SX25S004 specification summary, so acceptance limits must come from the original panel documentation and controller design.
When a high-capacitance cable is unavoidable, the design consideration is to control the signal return path, reduce unnecessary coupling, and validate the complete cable assembly rather than compensating blindly with stronger drive. Series damping, drive strength, termination, or edge-rate changes are system design decisions. They require verification for image stability, electromagnetic behavior, startup reliability, and controller output stress.
Power-up and shutdown should be observed together with the interface signals. Confirm that logic activity does not begin in an undefined state relative to the panel supply and bias rails. A visible flash, persistent dark segment, or incomplete frame after cycling power may involve sequencing, controller initialization, connector contact, or bias settling. Repeat the test with the original cable and a controlled replacement cable to establish whether the behavior follows the interconnect.
Mechanical installation matters during this test. Route the ribbon cable so that the bezel and rear cover do not impose concentrated bending or pulling force on the connector. Allow the frame to release vibration without transferring a sharp load into the glass edge or elastomeric contact. The correct retention method is determined by the original chassis design and should be verified after thermal cycling and equipment vibration testing.
For field service documentation, record the SX25S004 identification, panel technology, connector orientation, controller revision, cable construction, observed waveform condition, and environmental state. This creates a traceable basis for deciding whether the issue is in the LCD panel assembly or in the surrounding HMI electronics. Broader mechanical, optical, and electrical integration references are available in The Ultimate Guide to Industrial TFT LCD Technology, which can support comparative testing without changing the verified SX25S004 specifications.