Content last revised on October 10, 2026
2MBI100NB-120 Operational Boundaries: Evaluating Thermal Stress Alleviation in Bidirectional Limits
| Parameter | Official Specification |
|---|---|
| Manufacturer | Fuji Electric |
| Model | 2MBI100NB-120 |
| Product Category | IGBT Module |
| Rated Voltage | 1200.0 V |
| Rated Current | 100.0 A |
| Package | Fuji Power Module |
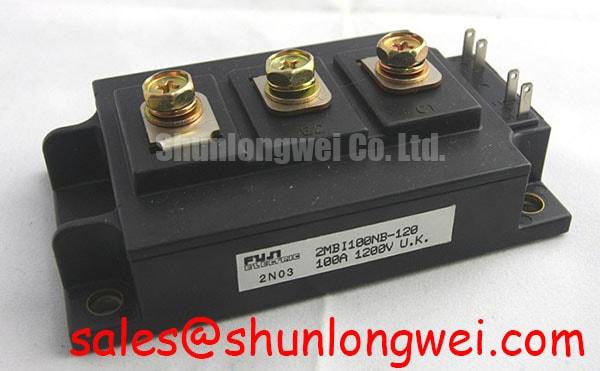
Measure the installed module’s cold-state terminal condition and compare the result with the approved phase-leg schematic before applying battery voltage or inverter DC-link power. The 2MBI100NB-120 is a Fuji Electric IGBT module with an official rated voltage of 1200.0 V and rated current of 100.0 A, housed in a Fuji Power Module package. These figures identify the device class; the allowable operating point in a commercial string inverter or micro-grid energy-storage converter remains dependent on switching frequency, cooling, current waveform, bus voltage, and the complete power-stage design.
In a bidirectional battery converter, the module may be evaluated in a phase-leg position where energy moves from the DC battery racks toward the inverter link during discharge and returns toward the battery during charging. That four-quadrant power-flow arrangement changes the thermal pattern from one-way operation to repeated heating and cooling. During peak shaving, the service engineer should correlate battery current, phase current, switching command, heat-sink temperature, and module case temperature across both charge and discharge events. A rising temperature difference between opposite operating directions can point to unequal gate timing, current sharing, diode conduction behavior, busbar asymmetry, or cooling-path variation rather than a single component fault.
Thermal stress alleviation begins with the mechanical interface. Clean the heat-transfer surfaces, inspect the mounting plane for distortion, and apply the selected thermal interface material consistently across the module footprint. The mounting arrangement should follow the Fuji Electric mechanical documentation for the package. A general industry design consideration is to tighten fasteners progressively in a cross pattern while preserving the specified flatness and torque requirements of the original assembly; the module case should not be used to compensate for a warped heat sink.
For a replacement assessment, compare the original circuit position rather than relying only on the current label. The linked 2MBI150N-120 has a different current designation and should be treated as a separate selection candidate requiring electrical, mechanical, thermal, and gate-drive review. It is not an automatic substitute for the 2MBI100NB-120.
In the front end of a storage inverter, the 2MBI75UA-120 may be encountered as a separately evaluated rectifier or auxiliary power-stage device. Its presence in the same system does not establish electrical interchangeability. Check the circuit topology, terminal assignment, isolation arrangement, protection coordination, and cooling path for each position.
During commissioning, inspect the temperature trend at matched operating points instead of judging performance from one brief current reading. If one direction of power flow produces greater thermal rise, first review dead time, gate resistance, current-sensor polarity, diode commutation, busbar symmetry, and heat-sink contact. Engineers evaluating a micro-grid energy-storage cabinet should also confirm enclosure airflow, fan control, dust loading, and ambient temperature because those conditions can shift the thermal margin without any change to the module rating.
2MBI100NB-120 Thermal-Electrical Optimization: Preventing Spurious Power-Up Shoot-Through Practical Tuning
Hold the high-voltage DC link in a safe, isolated state until the driver auxiliary supplies, UVLO interlocks, gate clamps, and controller inhibit signals have reached their defined operating condition. A half-bridge can produce unintended shoot-through when one gate becomes active before the complementary channel is properly held off. This risk is particularly important in a bidirectional converter because the control system changes the commanded energy direction while the power stage remains electrically coupled to the battery and inverter link.
A negative turn-off bias range of −5 V to −15 V is a design consideration for a suitable gate-driver architecture, not an official 2MBI100NB-120 rating. The system designer must verify whether the selected driver, isolation supply, gate-emitter voltage limit, clamp network, and board layout support the chosen negative bias. Do not apply a negative gate voltage simply because it is common in high-power switching designs. Check the original Fuji Electric documentation and the driver manufacturer’s limits before connecting the module.
Power sequencing should be checked with the control board disconnected from the high-voltage stage first. Confirm that the driver supply rises cleanly, UVLO remains asserted until the supply is stable, both gate outputs remain inactive during processor reset, and the fault latch behaves correctly after an auxiliary supply interruption. The enable path should be tested in both directions of commanded power flow, since a logic state that is safe during battery discharge may not produce the same interlock behavior during regenerative charging.
For high-side channels using isolated or bootstrap gate power, size the bootstrap capacitor from the actual gate charge requirement, driver quiescent current, charging interval, leakage, isolation-device consumption, and permitted gate-supply ripple. The required charge is not determined by gate charge alone. The selected value should be checked against the driver’s refresh duty cycle and the shortest available recharge interval. If the high-side supply droops during a long pulse or low-frequency operating region, UVLO may cycle and create abnormal switching transitions.
A practical bench sequence is to observe the driver outputs with the power devices unenergized, then introduce a controlled low-voltage test condition before connecting the full DC link. Compare the commanded dead time with the actual gate-to-emitter waveforms at the module terminals. Probe placement matters: a long ground lead can convert common-mode noise into an apparent gate spike. Use a measurement method suitable for isolated high-side nodes and verify that the probe’s common-mode rating exceeds the test condition.
⚠️ Field Alert: Disconnect the DC link and allow the specified discharge period before inserting, removing, or reworking any gate-drive or power-module connection.
Do not transfer thyristor trigger data such as IGT or VGT to this IGBT module. A storage converter may contain thyristors in another subsystem, but their pulse-trigger requirements belong to that thyristor stage. If a controller uses pulse trains for auxiliary thyristor firing, validate that circuit independently rather than treating it as a gate-drive specification for the 2MBI100NB-120.
Field Diagnostics & Commissioning: Mitigating Hard Switching Transients via a in 2MBI100NB-120 Topologies
Set the short-circuit protection path so that the controller detects an abnormal current event within the response window required by the complete power stage, while recognizing that a claimed response below 10 µs is a system design target rather than an official rating established by the listed product facts above. The short-circuit safe operating area, gate-driver delay, desaturation or current-sense filter, isolation delay, controller decision time, and turn-off profile must all be considered together.
Type-I and type-II short-circuit events should be distinguished by the operating condition that precedes them. A fault appearing immediately after turn-on may involve a hard load short, incorrect commutation, or inadequate current-sense response. An event that develops after normal conduction may involve saturation behavior, wiring inductance, gate disturbance, or a control-state transition. Use a controlled test fixture and suitable current and voltage probes to establish whether the gate command, collector-emitter voltage, and phase current remain time-aligned.
Two-stage soft turn-off is a design consideration used to reduce the electrical stress created when a faulted device is switched off abruptly. The first stage limits the gate discharge rate or transitions the device toward a controlled lower-current state; the second stage completes turn-off after the high-current condition has been reduced. The actual timing, gate resistance, clamp behavior, and fault threshold must be selected from the driver, module, bus inductance, and protection study. They should not be presented as fixed values for this Fuji Electric module.
Minimize the commutation loop area and keep the high-current path physically separated from sensitive gate and fault-sense traces. The design team should verify the peak collector-emitter voltage during turn-off against the DC-link voltage and the module’s official voltage rating. If the measured transient approaches the system boundary, review busbar geometry, local film-capacitor placement, snubber behavior, gate resistance, and the soft turn-off profile before increasing the nominal device rating.
The free-wheel diode’s reverse-recovery behavior can influence overshoot, common-mode current, and radiated EMI. A soft recovery factor is a system-level characteristic of the selected switching path and operating condition; it should not be assigned to the 2MBI100NB-120 without the relevant manufacturer data. Compare turn-on current rise, diode recovery current, DC-link ringing, and gate disturbance with a known-good power-stage waveform. If an EMI issue appears only during regenerative operation, examine the reverse-current commutation path rather than assuming that the IGBT itself is the sole source.
Fast semiconductor fuses may be coordinated with an IGBT module by comparing the fuse clearing behavior and the device short-circuit withstand characteristics. The I2t relationship, fuse voltage rating, prospective fault current, DC-link capacitance, and wiring inductance must be evaluated together. A fuse label alone does not establish protection against every hard-short event. Commissioning should include verification of the fault latch, contactor opening sequence, precharge state, and residual energy in the DC link.
Fuji Electric’s published information on 7th-Gen X-Series IGBT Modules and its Brake Chopper IGBT Modules can provide useful manufacturer context for semiconductor switching and protection evaluation. Those product families should not be treated as documentation for the 2MBI100NB-120 unless the applicable datasheet explicitly identifies the model.
Transient Dynamics & Electrical Design: Kelvin Emitter Connection on 2MBI100NB-120
Confirm the actual terminal drawing before attempting to separate an auxiliary emitter return from the main power emitter path. The listed product facts identify the 2MBI100NB-120 as a 1200.0 V, 100.0 A Fuji Power Module, but they do not establish a dedicated Kelvin emitter terminal. If the package drawing provides an auxiliary emitter connection, route the driver return directly to that point and keep it separate from the high-current emitter trace until the intended reference node is reached. If no such terminal is provided, the designer must use the documented power terminal arrangement and manage common-emitter inductance through layout and gate-loop control.
Emitter mutual coupling can disturb the apparent gate-emitter voltage when high current changes rapidly through a shared conductor. The gate driver then responds to a voltage that includes both the device’s actual gate-emitter behavior and the transient developed across the shared emitter path. Possible symptoms include gate ringing, unequal switching between parallel paths, false desaturation activity, or increased turn-off overshoot. These observations require waveform comparison at the module terminals and should not be assigned to a single internal failure without measurement.
Keep the driver supply return, fault-sense return, and gate-emitter reference away from the collector and emitter busbar current path. Use a compact gate loop, avoid routing the gate trace alongside high dv/dt collector nodes for long distances, and place clamp components according to the driver topology. The final spacing between high-voltage conductors must satisfy the applicable insulation, pollution, altitude, and enclosure requirements of the complete equipment. Creepage and clearance are system design properties, not values that can be inferred from the 1200.0 V label alone.
At the incoming bench stage, protect the module and measurement equipment from electrostatic discharge, identify the marked terminals from the approved drawing, and perform diode-mode checks only with the device isolated from capacitors, snubbers, gate supplies, and parallel semiconductor paths. A diode reading can help identify an unexpected open or short condition, but it does not prove dynamic switching health. Compare the cold-state result with a known-good reference using the same meter polarity, test leads, temperature, and discharge procedure.
💡 Bench Tip: Keep the module in an ESD-controlled area and record the cold-state terminal readings before mounting it into the converter, so later commissioning comparisons use the same baseline.
For gate-loop review, the Precision Gate Drive Design guide provides a related engineering reference on gate-drive layout and switching control. Use it as design guidance while retaining the Fuji Electric model documentation as the authority for the 2MBI100NB-120’s product-specific limits. When the completed power stage is tested, capture gate-emitter voltage, collector-emitter voltage, phase current, and driver fault status on the same time base. This makes it possible to distinguish a layout-induced transient from a sequencing error or a protection circuit that is responding later than intended.