Content last revised on September 10, 2026
DC-Bus Low-Inductance Laminated Busbar Design & Turn-Off Voltage Overshoot Suppression
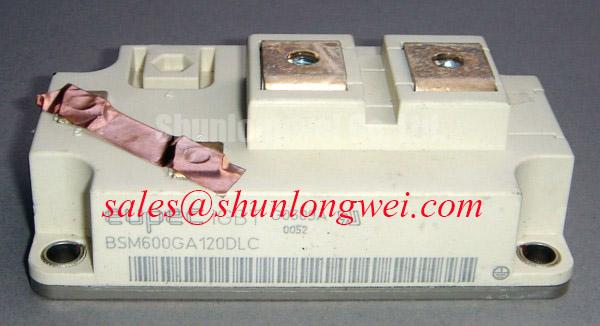
When troubleshooting high-speed rail and heavy freight locomotive traction inverters on the test track, turning off hundreds of amperes within fractions of a microsecond introduces brutal transient stresses. The BSM600GA120DLC IGBT module is rated at VCES = 1200V (Official Datasheet Specification) and handles a continuous current of IC,nom = 600A at TC = 80°C (Official Datasheet Specification), surging to IC = 900A at TC = 25°C (Official Datasheet Specification). Under emergency traction conditions or aggressive phase-controlled switching, parasitic inductance within the DC-link path transforms high di/dt events into severe collector-to-emitter overvoltage spikes.
Every field engineer who has inspected an exploded traction power block knows that exceeding the 1200V ceiling instantly punches through the silicon planar gate oxide. The peak transient turn-off voltage is directly governed by the sum of the DC-link operating voltage and the inductive overshoot, where the voltage spike equals the total loop inductance multiplied by the switch turn-off rate di/dt. In high-power locomotive traction cabinets operating at intermediate DC rail voltages of 600V to 750V, keeping the stray loop inductance below 25 nH is not an option; it is an absolute survival requirement for the module.
Achieving this low-inductance target requires wide, flat, and closely spaced copper plates in a laminated busbar topology. Planar busbars force the forward and return DC currents to flow in adjacent parallel planes, maximizing electromagnetic field cancellation. When retrofitting legacy traction stacks or servicing auxiliary converter assemblies, engineers frequently evaluate auxiliary half-bridge units alongside heavy main switches; for auxiliary inverter branches, the related FF150R12ME3G serves medium-power converter stages within distributed locomotive auxiliary power networks. For the main 600A traction arms powered by the BSM600GA120DLC, physical busbar clearances must strictly satisfy rail pollution degree standards (typically PD3 for traction under-chassis enclosures) through high-dielectric Kapton or Nomex insulation barriers.
Snubber configuration directly suppresses the residual parasitic inductance of the terminal bolts. Direct mounting of low-inductance polypropylene film snubber capacitors (typically 0.47 µF to 1.0 µF per module pair as a General Industry Design Consideration) directly across the positive and negative bus terminals clamps high-frequency ringing. Additionally, long motor leads extending from the traction converter to the under-truck bogie motors act as transmission lines. Without proper dv/dt output filtering or tuned dV/dt chokes, traveling voltage waves reflect at high-impedance motor terminals, doubling the peak voltage seen across stator windings and sending high-frequency common-mode noise back to the inverter module ground reference.
| Circuit & System Parameter | Datasheet Value / Engineering Boundary | Parameter Identity & Condition |
|---|---|---|
| Collector-Emitter Voltage (VCES) | 1200 V | Official Datasheet Specification (Tvj = 25°C) |
| DC Collector Current (IC,nom) | 600 A | Official Datasheet Specification (TC = 80°C) |
| Collector-Emitter Saturation (VCE(sat)) | 1.9 V (typ) / 2.4 V (max) | Official Datasheet Specification (IC = 600A, VGE = 15V) |
| Gate-Emitter Threshold (VGE(th)) | 5.0 V to 6.5 V | Official Datasheet Specification (IC = 24mA, VCE = VGE) |
| Thermal Resistance (RthJC) | 0.042 K/W | Official Datasheet Specification (per IGBT switch) |
| Thermal Resistance (RthCK) | 0.010 K/W | Official Datasheet Specification (with thermal grease) |
| Target Stray Busbar Inductance (Lσ) | < 25 nH | Design Consideration (High-Speed Traction Loop) |
Baseplate Convexity Compensation and Screw Tightening Sequence Guidelines
Thermal contact integrity determines whether a high-power traction module survives heavy freight start-up torque or enters catastrophic thermal runaway. The BSM600GA120DLC features a heavy copper baseplate designed with deliberate engineering convexity (pre-bowing). During manufacturing, the baseplate center is engineered with a microscopic crown. When bolted to a precision-machined heatsink, this curvature compresses the thermal interface material outward, driving air voids out toward the module perimeter and ensuring direct metal-to-grease-to-heatsink contact directly under the silicon dies.
When servicing traction inverters in depot workshops, applying thermal paste must follow strict physical parameters. Apply an even layer of high-grade silicone-based or synthetic thermal grease across the heatsink surface using a 75 µm to 100 µm calibrated screen stencil (Typical Starting Point for baseplate thermal interface application). Applying too much paste creates a thick thermal barrier, whereas applying too little leaves dry air pockets that produce localized hot spots. The factory-specified thermal resistance from case to heatsink is RthCK = 0.010 K/W (Official Datasheet Specification) when paired with thermal compound exhibiting a thermal conductivity of λ ~ 1 W/m·K.
⚠️ Field Alert: Never torque module mounting bolts to their maximum limit in a single circular pass. Uneven initial torque deforms the copper baseplate, permanently lifting the center of the module off the heatsink. Always execute a crosswise pre-tightening sequence using an M6 torque wrench set to 2.0 N·m (Design Consideration), followed by a final cross-pattern torque pass to 3.0–5.0 N·m (General Industry Design Consideration for M6 baseplate fasteners). Allow 15 to 30 minutes for the thermal compound to relax and squeeze out across the interface before applying full DC-bus voltage.
If retrofitting existing inverter assemblies where modern trench-gate components are being considered for fleet upgrades, engineers often benchmark mechanical footprint and loss profiles against newer platforms such as the FZ600R12KE4, which shares the 600A/1200V class rating while utilizing updated trench/field-stop architecture. Regardless of the module family installed, complementary gate interlock layout and dead-time management must prevent bridge shoot-through. For the BSM600GA120DLC, establishing a hardware-enforced dead time (tdead) of at least 2.5 µs to 3.5 µs (Design Consideration) ensures complete channel turn-off before the opposing rail arm is commanded high.
High-Speed Fault Management: VCE(sat) Desaturation Sensing Circuitry
In locomotive traction drives, motor winding insulation breakdown or wheel-slip induced phase shorts subject the power stage to sudden short-circuit conditions. The BSM600GA120DLC exhibits a nominal saturation voltage of VCE(sat) = 1.9V (typ) at IC = 600A, VGE = 15V, Tvj = 25°C (Official Datasheet Specification), reaching a maximum of 2.4V (Official Datasheet Specification). When a short circuit occurs, the collector current spikes violently, pulling the operating point out of saturation and into the active region, causing VCE to rise rapidly toward the full DC-link voltage.
Desaturation sensing circuits continuously monitor this collector-emitter potential during the on-state. The gate driver must detect the desaturation threshold and extinguish the gate signal within the short-circuit safe operating area (SCSOA) boundary, which is typically under 10 µs. A high-voltage blocking diode connected from the IGBT collector to the driver sensing pin isolates the low-voltage detection circuit during the off-state. Once the gate is commanded high, a blanking capacitor delays desaturation tripping for 1.5 µs to 2.5 µs (Typical Starting Point for blanking time tuning) to allow VCE to collapse fully past the switching edge without generating false fault trips.
For deep technical methodologies on static bench validation, gate-charge verification, and structural short-circuit diagnostics, engineers rely on comprehensive testing frameworks detailed in the Field Engineer’s Handbook. If the desaturation circuit triggers, abruptly pulling the gate from +15V to -8V under 3000A fault current induces a deadly di/dt voltage transient that will destroy the silicon. The driver must initiate a Two-Stage Soft Turn-Off (2-Stage STO), stepping the gate voltage down to approximately +7V to +9V to choke fault current smoothly before fully clamping the gate to its negative off-bias rail.
Bench testing an unmounted or suspect module requires systematic isolation checks. With an isolated digital multimeter on diode test mode, verify the internal anti-parallel freewheeling diode drop between C and E (typically 0.35V to 0.55V forward drop). Next, measure the gate-to-emitter resistance; a healthy module presents open-circuit impedance (>10 MΩ). Any measured resistance below 1 MΩ between gate and emitter indicates internal oxide puncture. Further verification of technological benchmarks across silicon generations can be referenced directly within the Infineon IGBT Modules & Discretes Official Portfolio.
Evaluating Thermal Capacitance vs Heat Sink Time Constant under Surge Bursts
Locomotive operations present severe cyclic thermal profiles. When a freight train accelerates a 4,000-ton cargo rake from a standstill on an incline, the traction inverter experiences massive low-frequency current bursts where thermal stress is concentrated heavily in the semiconductor chips rather than the liquid-cooled or forced-air heatsink. The junction-to-case thermal resistance for each switch in the BSM600GA120DLC is tightly controlled at RthJC = 0.042 K/W (Official Datasheet Specification).
Under short transient bursts (t < 50 ms), the bulk heatsink thermal capacitance has virtually zero impact on silicon junction temperature. The thermal energy generated by conduction and switching losses is absorbed almost entirely by the microscopic thermal capacitance of the silicon die, the solder layer, and the adjacent copper baseplate. To evaluate transient temperature rises during acceleration surges, thermal analysis utilizes multi-element RC Foster or Cauer network models. The transient thermal impedance Zth(j-c) climbs rapidly during the initial milliseconds of an overload event, demanding that dynamic junction calculations account for peak power dissipation rather than average thermal equilibrium.
The maximum junction temperature is rated at Tvj max = 150°C (Official Datasheet Specification). To ensure mechanical longevity under the thermal-mechanical stress of traction thermal cycling, operational guidelines establish a continuous running target junction temperature below 125°C (Design Consideration). Phase-controlled rectification at low motor fundamental frequencies (0.5 Hz to 5 Hz during initial train roll) concentrates current into single switch arms for prolonged fractions of a second, eliminating the phase-sharing benefit seen at high motor speeds.
When evaluating multi-module parallel assemblies in heavy locomotive converters, static and dynamic current sharing must be rigorously balanced. The positive temperature coefficient of the BSM600GA120DLC at higher current levels causes the hotter module to exhibit an increased VCE(sat), naturally shedding current to cooler parallel branches during continuous conduction. However, symmetric gate trace layout, identical gate loop impedances, and balanced busbar connections are mandatory to enforce dynamic current sharing during turn-on and turn-off transients, preventing localized current crowding and thermal overstress across the power array.