


Content last revised on October 17, 2026
Sharp LM8V301 Display Inspection and Replacement Considerations
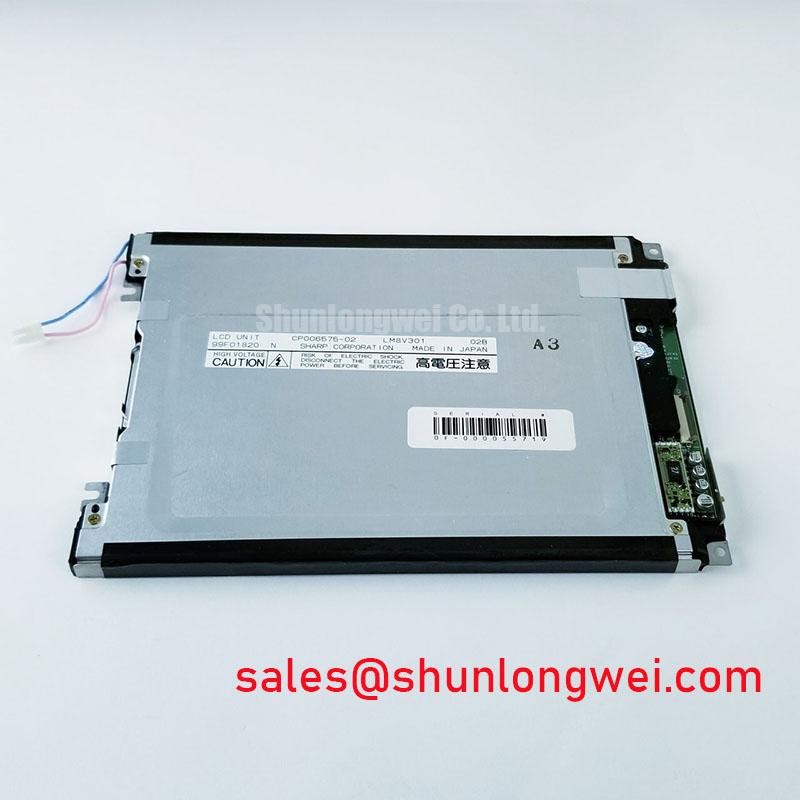
With the panel disconnected from the host controller, inspect the glass edge, flex connection, and bezel contact area before applying power. Inspect the illuminated viewing field only after confirming the electrical requirements. LM8V301 is identified as a Sharp monochrome passive-matrix LCD panel. The supplied product classification does not establish a confirmed operating-voltage, backlight-current, resolution, or connector pinout value, so those items should be matched against the original equipment documentation before replacement.
For marine radar displays, navigation bridge consoles, CNC operator panels, and industrial control interfaces, compatibility depends on more than the visible glass size. The receiving system must match the panel interface, bias arrangement, backlight circuit, mechanical aperture, and optical direction. Sharp’s display solutions portal and Sharp Devices Europe industrial display resources provide useful background when checking display integration practices.
HV Lead Wire Creepage Insulation and Secondary Transformer Corona Discharge Screening
For assemblies confirmed to use a CCFL backlight, high-voltage wiring should be inspected with power disconnected and with the secondary transformer, lead routing, and lamp connection examined as one insulation system. Values such as 1200–1600 Vrms for ignition and 300–600 Vrms during sustained operation are illustrative of some legacy CCFL assemblies, not official LM8V301 ratings or suitable screening test voltages without supporting documentation. Likewise, a tube-current target of 5.0 mA ± 0.5 mA should only be applied when it is specified by the original backlight inverter or panel documentation.
During a replacement assessment, look for carbonized insulation, displaced high-voltage leads, sharp chassis edges, and contamination around the transformer secondary. A cold-start arc can leave intermittent damage that is not visible during a short low-load test. Keep the high-voltage path physically separated from signal wiring and use the original insulation barriers where the equipment design provides them. The final clearance and creepage arrangement remain system-level design considerations governed by the enclosure, pollution environment, operating voltage, and applicable safety standard.
Optical inspection should take place after the panel has reached a stable operating condition. Check whether the polarizer shows local yellowing, edge darkening, or heat-related contrast loss. In bright bridge-console lighting, reflective ambient contrast can make a weak backlight appear functional while text remains difficult to read. Sub-zero operation introduces a separate concern: liquid-crystal response can become visibly slower as viscosity changes with temperature. A controlled cold soak within the documented operating limits and a moving-character test are more informative than a static screen photograph.
⚡ Safety Interlock Note: Disconnect the inverter supply and allow the high-voltage section to discharge before removing the backlight connector or handling the panel.
4-Bit and 8-Bit Digital Parallel Bus Timing: Frame Sync, Line Pulse and Shift Clock
Legacy monochrome panels using parallel video control require the host timing signals to be identified by function rather than by connector position alone. FLM establishes frame synchronization, LP marks the line transfer event, and CP shifts pixel data into the panel interface. Whether the panel uses these signals and whether the host operates a 4-bit or 8-bit path must be confirmed from the original panel and controller documentation, because an apparently compatible connector can still produce incorrect text, unstable rows, or a blank display.
Use a known-good controller or service fixture when comparing signal order and timing. Observe the relationship between FLM, LP, and CP at the panel connector, then compare the data transition window with the clock edge. Excessive cable length, poorly referenced grounds, or routing beside servo wiring may introduce clock jitter or intermittent line errors. A 100 Ω differential-pair rule is relevant to LVDS systems, but it should not be transferred to a parallel passive-matrix interface unless the host equipment actually contains an LVDS link upstream.
Power sequencing also deserves attention. For systems using a separate negative contrast or bias rail, follow the documented startup and shutdown sequence; the logic rail typically needs to establish a valid state before that bias rail is enabled, and shutdown should avoid leaving a bias voltage active after the logic supply has collapsed. The often-used VEE/V0 range of −15 V to −24 V is an engineering reference for some legacy STN systems, not a confirmed LM8V301 specification. Ripple on that rail can appear as contrast breathing, uneven characters, or a display that changes with screen content. Designers should verify the actual bias voltage, polarity, ripple, and any thermistor compensation from the original display circuit.
For a replacement involving a related display architecture, engineers may compare the mechanical and interface requirements of LM64P11. This is a neutral cross-reference for evaluation, not a prescriptive substitute for LM8V301.
Polarizer Delamination Bubble Mitigation and Optical Retardation Film Inspection under Workshop Lighting
Inspect the active area at several viewing angles with the display unpowered, then repeat the inspection under uniform illumination after operation. Bubbles, crescent-shaped edge lifting, haze, and localized color changes can indicate aging of the polarizer or adhesive layer, but the visible symptom should be compared with the panel’s normal optical behavior before a replacement decision is made.
Legacy transflective displays can lose practical contrast when ultraviolet exposure, heat, or prolonged high ambient illumination affects the polarizer. A workshop lamp placed directly above the glass may hide low-contrast text by creating reflections, while oblique illumination can reveal surface lifting that is not visible straight on. Record the condition of the full field, including corners and the area around the bezel, rather than judging only the center characters.
Optical checks should be coordinated with the digital interface test. A display with acceptable static contrast can still show missing rows if CP jitter, LP placement, or FLM timing is marginal. Where these signals and a separate negative bias rail are used, check the logic sequence with the controller connected and confirm that the logic supply is established before the negative bias rail, as required by the panel documentation. This reduces the possibility of applying an invalid bias state during startup, while the system engineer remains responsible for validating the actual timing and voltage limits.
For broader service guidance on industrial display selection, optical inspection, and legacy interface evaluation, consult The Ultimate Guide to Industrial TFT LCD Technology. Its TFT-specific interface guidance should not be assumed to apply to a passive-matrix panel.
Cleaning PCB Gold Contact Pads and Inspecting Zebra Rubber Strips
When rows or columns disappear, inspect the panel connections rather than pressing harder on the glass. If the assembly uses a serviceable elastomeric zebra connector, contamination, vibration displacement, or uneven bezel loading can interrupt selected conductive paths. Remove power, follow the equipment’s disassembly procedure, release the mechanical clamp evenly, and document the original connector position before cleaning. Do not attempt to remove bonded flex connections as though they were removable zebra connectors.
Anhydrous IPA may be used sparingly on suitable PCB gold contact pads with a lint-free swab, followed by complete evaporation, where permitted by the service documentation. Do not flood the zebra rubber strip, scrape the conductive faces, or introduce abrasive material into the connector interface. Reinstall the strip squarely across the contact field, ensuring that its alignment has not shifted sideways. Use the original clamp geometry and documented assembly requirements to control compression; no LM8V301-specific contact-pressure value is established here.
After reassembly, test a full screen of solid black, solid white, vertical bars, horizontal bars, and normal text. These patterns help distinguish a local contact problem from a controller timing issue without assuming a single cause. If the panel is installed near a variable-frequency drive or servo amplifier, route the display cable away from high-current switching paths and verify the ground reference at both ends. Another display model, such as LM24010Z, may be evaluated separately, but its function and electrical requirements must not be assumed to match the LM8V301 assembly.
💡 Bench Tip: Use ESD protection, keep removable connectors correctly aligned during reassembly, and secure the bezel only after the contact area is centered.


