Content last revised on September 13, 2026
Wide Temperature Operational Margin and Sub Zero Liquid Crystal Response
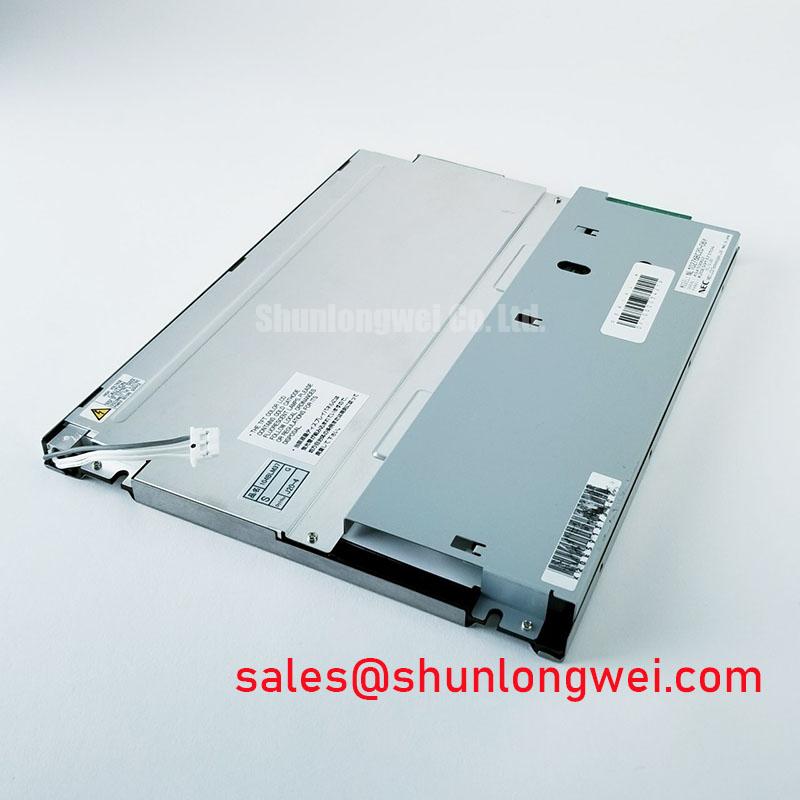
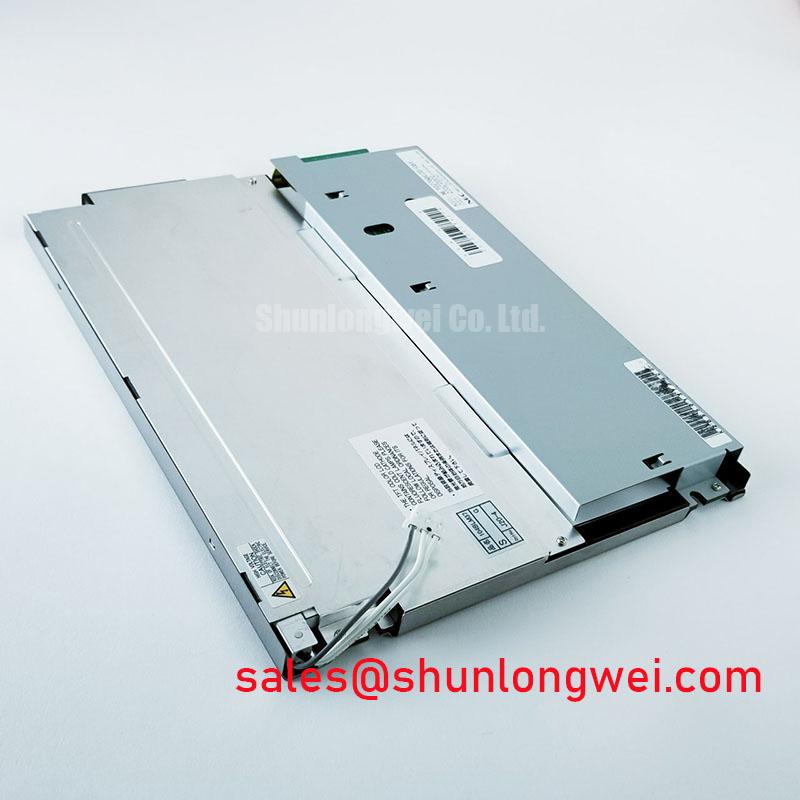
Before connecting the replacement panel, inspect the NL10276AC30-53D for visible damage, compare its connector and mounting features with the removed display, and confirm the original equipment documentation before applying power. The available factory information identifies this unit as an NEC industrial grade LCD/HMI panel with a TFT LCD display module construction. The supplied factory data does not confirm a complete electrical pinout, display resolution, brightness rating, backlight type, supply voltage, operating temperature range, or interface mapping, so those items must be checked against the original panel documentation or an authorized technical datasheet.
The NL10276AC30-53D may be evaluated for industrial HMI assemblies, equipment monitoring panels, and telematics displays used in demanding mobile machinery. A heavy mining shovel or earthmoving equipment cab can expose a display assembly to vibration, rapid temperature transitions, dust ingress, and repeated connector movement. Those conditions make the mechanical installation and interface verification just as important as the visible image quality.
The requested temperature range of −30°C to +85°C must not be treated as an official rating for this model because it is not included in the supplied factory parameter set. It is appropriate to treat that range as a system validation condition only when it is specified by the equipment manufacturer. At sub zero temperatures, liquid crystal response can become slower, which may appear as delayed gray transitions or motion smearing during cold startup. This behavior is not, by itself, sufficient to identify a defective panel. Engineers should compare the cold image response with a known good unit while monitoring the panel supply, video timing, and backlight behavior.
Thermal cycling also places stress on the bezel, connector retention system, flexible cable, and mounting points. The display should be supported evenly around its designed mounting area rather than pressed against the active viewing surface. The enclosure should provide sufficient clearance for the flexible circuit and should not force the cable into a sharp fold. Where the panel is installed in a vibrating cab, the system designer should evaluate how the bezel and chassis transfer shock into the glass and connector area. The final damping method remains equipment specific and must be verified through the machine manufacturer’s vibration and shock test plan.
High EMI environments require a controlled signal return path. A commonly used design consideration for LVDS routing is a differential characteristic impedance of 100 ohms with a tolerance of ±10 percent, but this is a board and interconnect design target, not an official electrical specification for the NEC panel. Pair geometry, reference plane continuity, connector construction, and cable length should be assessed together. Engineers should also verify pair skew against the source controller and the original display assembly rather than applying an assumed universal limit.
FPC handling deserves a separate inspection. Before insertion, check that the cable is fully aligned with the connector, that the locking mechanism is open during insertion, and that the exposed contacts are clean and undamaged. A cable that appears connected can still have incomplete contact if the lock is not fully engaged. Repeated bending during service can also change contact stability without leaving obvious marks. The replacement process should therefore record the cable bend direction and the original routing before the old panel is removed.
VESA and JEIDA Data Mapping Alignment
Image mapping must be verified at the system level because the supplied factory information does not provide a confirmed LVDS or TTL pin assignment for this specific unit. The integrator should not assume that a compatible connector shape guarantees compatible electrical mapping. The source controller documentation should identify the required logic supply, signal format, pixel clock arrangement, channel order, and data mapping before the panel is powered.
JEIDA and VESA mapping differences can produce incorrect color order, split images, abnormal gradients, or unstable synchronization even when the panel illuminates. A field replacement test should begin with the original controller and a known good cable wherever possible. Compare the displayed color bars, grayscale steps, full screen patterns, and moving test images. If the image is divided, shifted, or intermittently lost, inspect the channel assignment, clock polarity, cable seating, grounding, and controller configuration as a group rather than assigning the symptom to one cause.
Power sequencing is another important compatibility check. The required supply voltage for the NL10276AC30-53D is not included in the supplied official parameter summary. The system integrator should verify the required supply voltage from the original panel documentation. The same verification applies to enable signals, reset behavior, backlight control, and any power good interlock. A replacement panel should not be connected to an assumed 3.3 V or 5 V rail without documentary confirmation.
During bench testing, measure the supply at the panel connector while the display is starting and while the backlight changes state. Observe whether the controller output becomes active before the panel supply has stabilized. White screen behavior, a dark image, or repeated startup can involve timing interaction between the host board, panel logic, and backlight driver. An oscilloscope comparison with the original signal path can help distinguish a timing issue from a connector or panel fault. The equipment designer must define acceptable rise time and sequencing margins from the complete system specification.
Signal integrity depends on the entire transmission path, including the controller output stage, board traces, cable, connector, and panel input. Keep differential pairs referenced to a continuous return path and avoid unnecessary stubs. Pair polarity should be checked against the original assembly, especially after cable replacement. When a high EMI environment is expected, test the display while nearby motors, contactors, inverters, or switching supplies operate in their normal states. The panel itself should not be described as independently certified for whole equipment EMC compliance.
💡 Pro Tip: Keep each differential pair routed as a matched physical path and verify image stability with the actual equipment harness installed, not only with a short bench cable.
For cross reference work, engineers can review the mechanically related NL10276BC16-06 as a separate product record. It should be compared using documented dimensions, connector position, interface mapping, and optical requirements rather than selected solely because the modules appear similar.
Constant Luminance Control and Backlight Reliability Verification
The supplied factory information classifies the NL10276AC30-53D as a TFT LCD display module but does not confirm whether the installed backlight is LED or another technology. The system integrator should verify the original backlight architecture, driver interface, current requirements, dimming method, and connector pinout from the equipment documentation. A visually similar replacement cannot be assumed to accept the same backlight control signal.
Backlight evaluation should begin with uniformity across the active area. Display a neutral gray or white test pattern and inspect the corners, edges, and center under controlled ambient lighting. Uneven luminance can result from optical aging, driver regulation, mechanical pressure, cable issues, or differences in the controller image settings. A comparison against the removed panel is more useful than relying on an unverified nominal brightness value.
Thermal management should be considered around the complete display assembly. If the equipment enclosure includes metal rails or a heat spreader, the designer should confirm that those parts support the frame without loading the glass or blocking ventilation paths. Localized heat near the display edge can affect backlight behavior and enclosure reliability. The correct thermal interface, contact pressure, and heat path must be determined from the equipment structure and validated under the intended ambient conditions.
Terms such as L70 and B50 describe a test methodology or reliability reference, not a confirmed rating for this NEC model in the supplied data. No specific half life, lumen maintenance figure, or LED failure distribution should be assigned to the NL10276AC30-53D without the relevant manufacturer documentation. For a repair decision, record the initial luminance, operating mode, ambient condition, and driver settings, then repeat the measurement after the equipment’s defined validation interval.
Dimming control should be checked for visible flicker, camera banding, audible noise, and interaction with the host controller. If pulse width modulation is used, the designer should verify the permitted control frequency and duty behavior from the backlight driver documentation. The display module’s classification alone does not establish a PWM frequency range or a guaranteed dimming linearity. A stable current regulated driver and clean control reference are important, but the final selection belongs to the system design.
Long term static HMI content also deserves attention. Fixed logos, status bars, and machine diagrams can create uneven aging or temporary image retention depending on the panel technology, drive conditions, temperature, and operating schedule. Equipment software can reduce continuous stress by varying static content where the application permits. This is a design consideration rather than a model specific guarantee. The service team should distinguish temporary retention from permanent luminance nonuniformity by using controlled patterns and allowing the display to return to a normal operating state before making a replacement decision.
For a broader explanation of industrial TFT panel interfaces, optical behavior, and selection factors, refer to The Ultimate Guide to Industrial TFT LCD Technology. The article can support the preliminary evaluation, while the original NEC documentation remains the authority for model specific electrical limits.
Acoustic Noise and EMI Evaluation During Backlight Switching
Backlight noise should be investigated at the driver and enclosure level rather than attributed automatically to the LCD glass. The supplied factory parameters do not confirm a CCFL inverter, LED driver, ignition voltage, PWM range, dimming ratio, or acoustic specification for the NL10276AC30-53D. The original equipment wiring should therefore be inspected before choosing a replacement driver or changing the dimming method.
If the original assembly uses a high voltage lamp inverter, the service procedure must follow the equipment manufacturer’s isolation and discharge requirements. If it uses an LED driver, the designer should verify constant current regulation, enable polarity, fault reporting, and the permitted dimming input. These architectures are not interchangeable simply because both produce panel illumination. The connector pinout and driver feedback arrangement require documentary confirmation.
Audible noise can be influenced by magnetic components, switching frequency, mechanical resonance, mounting pressure, and enclosure panels. A practical evaluation compares the display at several normal brightness settings while recording whether the sound changes with PWM command, supply loading, or cabinet vibration. Do not use a tonal change alone as proof of a component failure. Correlate the acoustic observation with backlight current, supply ripple, image stability, and connector condition.
EMI testing should be performed with the complete display assembly installed in its intended cable routing and enclosure. The test should include normal controller activity, backlight transitions, maximum brightness, minimum brightness, and any communication equipment operating nearby. Minimize unnecessary loop area in power and backlight wiring, maintain a defined return path, and keep sensitive video pairs away from noisy switching nodes. These are general design considerations; compliance with CISPR, EN 55011, or another equipment standard belongs to the finished system and cannot be claimed for the display module alone.
For field replacement, document the original cable length, shield termination, chassis bonding, and connector clamp arrangement before dismantling the panel. After installation, inspect the image during equipment startup, warm operation, cold operation where specified by the machine builder, and active backlight dimming. A panel that passes a short bench test can still require additional assessment after the complete harness, enclosure, and control software are restored.
The available product record supports identification of the NEC NL10276AC30-53D as an industrial grade TFT LCD display module. Final approval for a heavy mining shovel, earthmoving equipment telematics display, or another industrial HMI should be based on verified mechanical drawings, original interface documentation, electrical limits, backlight requirements, and equipment level environmental testing.