Content last revised on September 10, 2026
2MBI300VH-170-50 Thermal Electrical Optimization: Baseplate Thermal Grease Layer Control Practical Tuning
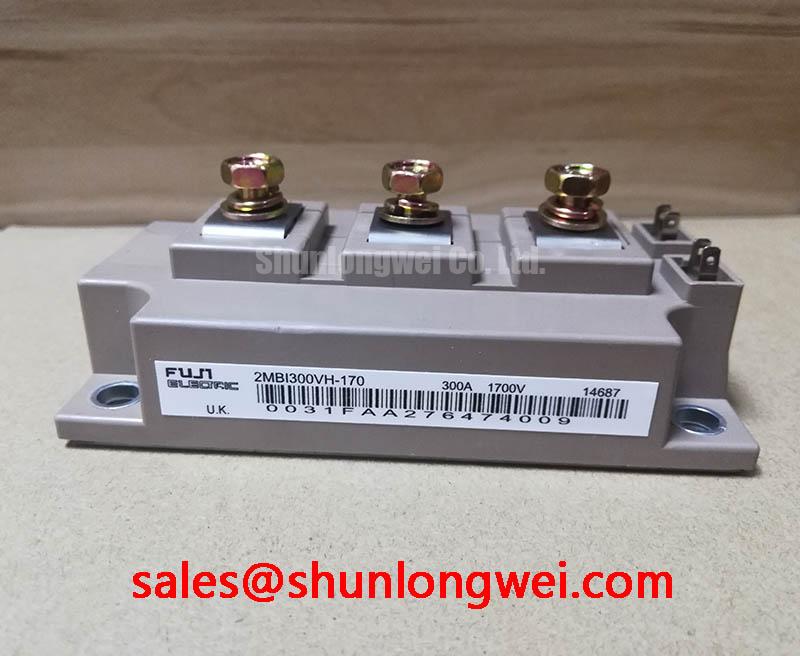
Remove the previous thermal interface material completely before placing the replacement module on the heatsink. A clean, flat contact surface helps prevent local air pockets and uneven pressure. The thermal compound should be applied as a uniform, thin layer appropriate to the selected material. The supplied engineering guidance identifies a practical interface thickness range of 50 to 100 μm; this is an Engineering Recommendation, not an official electrical rating of the module.
Check the heatsink for burrs, contamination, excessive curvature, or damage around the mounting holes. A curved heatsink can concentrate mechanical force near one section of the baseplate while leaving another section with poor thermal contact. Engineers should confirm flatness using the equipment manufacturer’s service specification and correct the mechanical interface before applying final clamping force.
Use a crosswise tightening sequence so that the baseplate seats progressively rather than being pulled down from one corner. The final torque must follow the fastener size, washer arrangement, heatsink material, and module manufacturer documentation. Do not treat a general M5 torque value as a guaranteed parameter for this specific module. After installation, inspect the compound spread at the accessible edges and confirm that the power terminals remain free from mechanical strain.
Thermal troubleshooting should start with an infrared comparison between equivalent switching positions, followed by checks of heatsink airflow, coolant or fan operation where applicable, and the temperature sensor path. A temperature difference between parallel positions may involve contact pressure, current imbalance, gate timing, or measurement placement, so the complete power stage should be evaluated rather than assigning the symptom to the module alone.
Field Alert: Disconnect the DC link and gate drive supply before inserting or removing the module, and follow the equipment’s discharge verification procedure.
2MBI300VH-170-50 Circuit Protection and Reliability: Calibrating Symmetrical Busbar Geometry for High Current
The 300.0 A rating is an official product specification, but the usable current in a traction inverter remains system determined. Busbar resistance, commutation inductance, cooling performance, switching duty, overload profile, and protection response all affect the actual operating margin. When engineers evaluate the device for a high-speed rail or heavy freight locomotive traction inverter, they should compare the existing electrical topology with the module’s original application documentation.
Parallel module arrangements require particular attention to both static and dynamic current sharing. The positive temperature coefficient commonly associated with IGBT conduction voltage can support static sharing under suitable conditions, but it does not remove the need for matched thermal paths and symmetrical conductor resistance. This statement is a Design Consideration, not a guaranteed sharing characteristic for every assembled system.
Keep the DC bus and emitter return paths physically balanced where parallel devices are used. Gate wiring should have comparable length, routing, return impedance, and coupling environment. Gate resistors, driver output capability, dead time, interlock behavior, and desaturation response must be checked as a complete circuit. Designers should verify turn on and turn off timing on each branch with an oscilloscope before applying full operating voltage.
A complementary rectifier stage may be evaluated separately in the same power conversion system. The 2MBI150UC-120 can be reviewed as a neutral reference for a related rectifier position, but electrical substitution requires confirmation of voltage, current, circuit function, thermal interface, and terminal compatibility.
For protection development, the gate driver should prevent cross conduction through correctly coordinated interlock and dead time. The actual delay must be established from switching waveforms, propagation tolerances, device temperature, and the driver design. A desaturation circuit with soft shutdown may reduce electrical stress during a short circuit, but the protection threshold, blanking behavior, shutdown slope, and short circuit withstand capability must be verified from the applicable Fuji Electric documentation and system test results.
Field Diagnostics and Commissioning: Dynamic Power Loss Dissipation and Multi R in 2MBI300VH 170 50 Topologies
During a failed-unit investigation, begin with a visual inspection of the case, terminals, mounting surface, and nearby snubber or gate-drive components. With the power removed and the DC link confirmed discharged, compare cold-state impedance readings between equivalent terminals and against a known-good module or documented service baseline. These readings are screening observations, not pass or fail limits unless the manufacturer specifies them.
Next, verify the gate driver supply, command waveform, gate return path, and isolation barrier. An unexpected gate waveform may reflect a driver fault, common-source or emitter inductance, damaged isolation, excessive coupling, or an incorrect reference connection. Compare the suspected phase with a healthy phase using the same probe type, bandwidth, ground method, and measurement location.
Dynamic loss should be assessed from the actual switching waveform and load profile. Conduction loss is related to the device’s voltage drop and current, while switching loss depends on voltage, current, transition behavior, gate drive, temperature, and commutation conditions. The official information supplied for this product confirms the 1700.0 V voltage rating, 300.0 A current rating, and module package, but it does not establish a universal system loss value.
For pulsed overload analysis, engineers may use a multi RC transient thermal model to estimate junction temperature from measured power pulses and the applicable junction to case thermal data. This is an Engineering Calculation and requires the correct thermal impedance curve, pulse duration, duty cycle, case temperature, and mounting condition from the relevant datasheet. The calculated result should then be checked against measured case temperature and switching behavior.
Do not infer short circuit capability, safe operating area, cosmic ray tolerance, single event burnout performance, FIT rate, altitude derating, or operating life from the current and voltage ratings alone. Those subjects require device specific manufacturer data, recognized reliability methods, or a qualified application test. The IGBT Design & Integration reference can support broader review of gate drive, thermal management, and circuit integration principles.
In phase controlled rectifier systems, conduction angle and firing synchronization influence input current distortion and high order harmonics. Engineers should assess the complete line impedance, transformer arrangement, control strategy, filtering, and applicable railway or industrial power quality requirements. The IGBT module itself should not be presented as independently certified for complete equipment EMC compliance. Fuji Electric’s Brake Chopper IGBT Modules page provides manufacturer context for related power semiconductor applications.
Benchtop Waveform Tuning: Mitigating Stress via High Frequency Commutation Loop Inductance on 2MBI300VH 170 50
Use a differential voltage probe and a properly referenced current probe to observe the switching node, gate signal, and commutation current together. The objective is to identify overshoot, ringing, unequal branch timing, and excessive gate oscillation before reconnecting the full equipment load. Probe loop area should be minimized because the measurement arrangement can otherwise introduce ringing that is not present in the power circuit.
Commutation loop inductance should be minimized through short, wide, closely coupled forward and return conductors. Symmetrical planar busbar geometry can reduce unequal parasitic impedance between parallel paths, but the acceptable inductance is system determined by DC link voltage, current slew rate, switching speed, insulation spacing, and the module layout. The system engineer must verify peak voltage margins during switching tests rather than applying an assumed universal limit.
The relationship between switching overshoot and parasitic inductance can be used as an Engineering Calculation: the transient contribution rises with commutation inductance and current rate of change, so reducing loop inductance or controlling the current transition can lower the observed peak. Snubber selection should be based on measured ringing frequency, energy, capacitor voltage rating, pulse current, resistor loss, and thermal performance. A fixed capacitor value should not be prescribed without those circuit measurements.
When commissioning a traction inverter, tune the gate network with the actual busbar, driver, load, and temperature conditions. Confirm dead time, soft shutdown behavior, turn off voltage, and diode or complementary path commutation at the intended operating points. Engineers should also check whether a control change intended to reduce switching loss creates additional voltage stress or electromagnetic coupling.
The 2MBI300U4H-120-50 may be reviewed as a related Fuji Electric module reference during a compatibility study. It should not be treated as an automatic substitute for the 2MBI300VH-170-50. Mechanical fit, electrical ratings, gate characteristics, thermal data, protection coordination, and equipment approval must be established before any interchange decision.