
Content last revised on October 9, 2026
Optical Luminance Degradation Curve and CCFL to LED Modernization Retrofit Pathways
| Model | KG057QV1CA-G20 |
| Manufacturer | Kyocera |
| Product Category | Industrial Grade LCD/HMI Panel |
| Display Construction | TFT-LCD Active Matrix Color Display Module |
| Specification Status | Decoded Baseline / Standard Form Factor |
| Resolution, supply, interface and backlight data | Consult the applicable panel documentation before system integration |
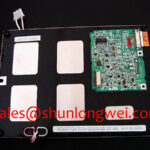
Begin incoming inspection by displaying full white, black, red, green and blue test fields across the KG057QV1CA-G20, then inspect the active area for dead pixels, stuck pixels, uneven luminance and visible edge shading. The confirmed product identity is a Kyocera TFT-LCD Active Matrix Color Display Module; the available baseline does not establish a particular backlight technology, so a CCFL to LED conversion must be treated as a system retrofit rather than an inherent feature of this model.
For a replacement panel used in a protection relay interface or SCADA dispatch console, record the original display’s brightness impression, color balance and dimming behavior before removal. A retrofit evaluation should compare the replacement backlight driver, connector arrangement, optical stack and mechanical clearance with the original assembly. A constant current LED driver can offer stable brightness control, but its current regulation, open circuit response, short circuit response and PWM behavior remain properties of the selected driver and system design.
The often quoted 50,000 hour point at 50 percent brightness is a common industry lifetime reference for LED backlight evaluation, not an official lifetime rating established here for this Kyocera model. Designers should request the relevant backlight curve and test conditions when luminance retention is important. Ambient temperature, drive current, enclosure heat and duty cycle can shift the observed decay curve. The Kyocera Industrial TFT-LCD Display Technologies reference provides useful background for assessing industrial display technologies without assigning unverified performance values to this specific part.
When evaluating PWM dimming, inspect the panel image with a photodetector or high-speed camera rather than relying only on visual judgment. A proposed control range such as 200 Hz to 1 kHz may be a suitable engineering test window for a selected LED driver, but it is not a factory specification for the KG057QV1CA-G20. Check visible flicker, camera banding, driver audible behavior and brightness uniformity at several duty settings.
Aluminum Heat Spreader Sizing and Thermal Interface Placement along Narrow Display Edges
Map temperature around the display frame, backlight region and narrow edge zones while the panel operates in its intended enclosure, because localized heat can affect optical uniformity and long term interface stability. The standard form factor classification identifies the mechanical baseline, but it does not define an approved aluminum rail size, thermal interface material or enclosure cooling method.
As a Design Consideration, an aluminum spreader should contact the intended heat transfer surface without pressing against the active display area, polarizer or flexible connections. The rail should distribute heat rather than create a concentrated mechanical load. Thermal pads, tapes or compounds should be selected for compression behavior, electrical insulation requirements and compatibility with the surrounding assembly. The system engineer should validate the result by comparing edge temperature, center temperature and image uniformity during warm operation.
Heat management also affects signal integrity. If a TTL or LVDS transmitter is installed near a warm display edge, check clock quality, data hold behavior and receiver margin across the complete operating temperature range specified by the host equipment. These electrical limits belong to the controller, cable and receiver combination unless the panel documentation states otherwise. A display that appears optically uniform at room temperature can still show intermittent artifacts when connector strain, temperature drift or cable movement changes the signal path.
For a high voltage substation protection or SCADA console, the practical compatibility check includes bezel clearance, rear cable routing, service access and airflow around the display assembly. A compatible mechanical envelope does not by itself confirm electrical interchangeability. Engineers comparing other panel families can review the LQ10D131 listing as a separate same class evaluation reference, while confirming connector and timing requirements independently.
Controlled 100 Ohm Differential Impedance Flex Routing to Suppress High Frequency Jitter
Inspect the display cable path for sharp bends, uneven insertion and shield discontinuity before investigating image artifacts. Split screen effects, unstable columns or intermittent synchronization can involve mapping, timing, power sequencing, cable construction or connector seating, so the signal path should be compared with a known good assembly using an oscilloscope and the host controller documentation.
A controlled 100 ohm differential route is a Design Consideration for systems using differential display signaling; it must be confirmed against the actual interface standard and cable construction. Do not assign a JEIDA or VESA mapping to the KG057QV1CA-G20 without the matching panel documentation. The integrator should verify lane order, color depth, clock polarity, enable timing and connector pin assignments before applying power.
Power sequencing deserves the same attention. The system integrator should verify the required logic supply voltage from the original panel documentation rather than assuming a general 3.3 V or 5.0 V interface. During bench testing, observe the supply rise, display enable timing and backlight activation together. If the image appears only after repeated power cycling, compare the controller’s sequence with the panel requirements and inspect the cable for marginal contact.
Backlight faults should be separated from video faults. A dark image with valid video data can direct attention toward the backlight driver, enable signal or protection response, while a lit panel with corrupted geometry points toward data mapping or timing. This distinction supports faster repair without assigning a single cause to every symptom. Keep the differential pair geometry consistent through the flex transition, minimize unnecessary stubs and validate the completed assembly under vibration and temperature conditions representative of the equipment.
💡 Bench Tip: Use ESD protection during inspection, keep the flex cable square to its connector, and lock the retainer evenly before applying power.
Polarizer Durability and Optical Retardation Film Inspection under Direct Industrial Lighting
Inspect the display under the actual lighting direction of the equipment, because direct overhead light can reveal surface haze, reflections, pressure marks and nonuniform viewing behavior that are difficult to see on a dark bench. The active matrix color construction is confirmed for this model, while polarizer type, retardation film structure, anti glare treatment and viewing angle values require the applicable panel documentation.
For an industrial HMI, compare the image from the operator position, service position and oblique positions used during maintenance. TN, IPS and MVA technologies can produce different grayscale and viewing responses, so a replacement should be judged against the original operating requirement rather than a generic viewing angle claim. The Amorphous Silicon TFT Technology reference offers general technology context, but it should not be used to infer unlisted optical properties of this Kyocera module.
Use white and mid gray fields to inspect luminance uniformity, then use dark fields to identify glow, edge leakage or pressure-related disturbances. Avoid pressing the viewing surface during cleaning or assembly. Select an enclosure window and surface treatment that reduce reflected light without introducing a visible haze layer. AG and AR treatments are system-level optical choices unless explicitly included in the panel specification.
Cold-temperature testing should focus on image response, startup behavior and grayscale transitions after the complete assembly reaches the target environment. Liquid crystal response can change with temperature, but the appropriate compensation, heater arrangement and control sequence must be determined by the equipment designer. Do not present a heater strip as a standard feature of this model. For long-term test planning, the The Ultimate Guide to Industrial TFT-LCD Technology provides broader selection and integration context.