Content last revised on October 27, 2026
Field Diagnostics and Commissioning: DBC Micro Crack Screening in CM600DY-34H Topologies
- Confirm terminal to baseplate insulation using the equipment manufacturer’s approved insulation test procedure before energizing the assembly.
- Check the mounting surface, thermal interface, and clamping alignment across the complete module footprint.
- Inspect gate drive isolation, auxiliary emitter routing, and connector polarity before connecting the power circuit.
- Record the installed module rating against the inverter DC link, braking duty, and switching test plan.
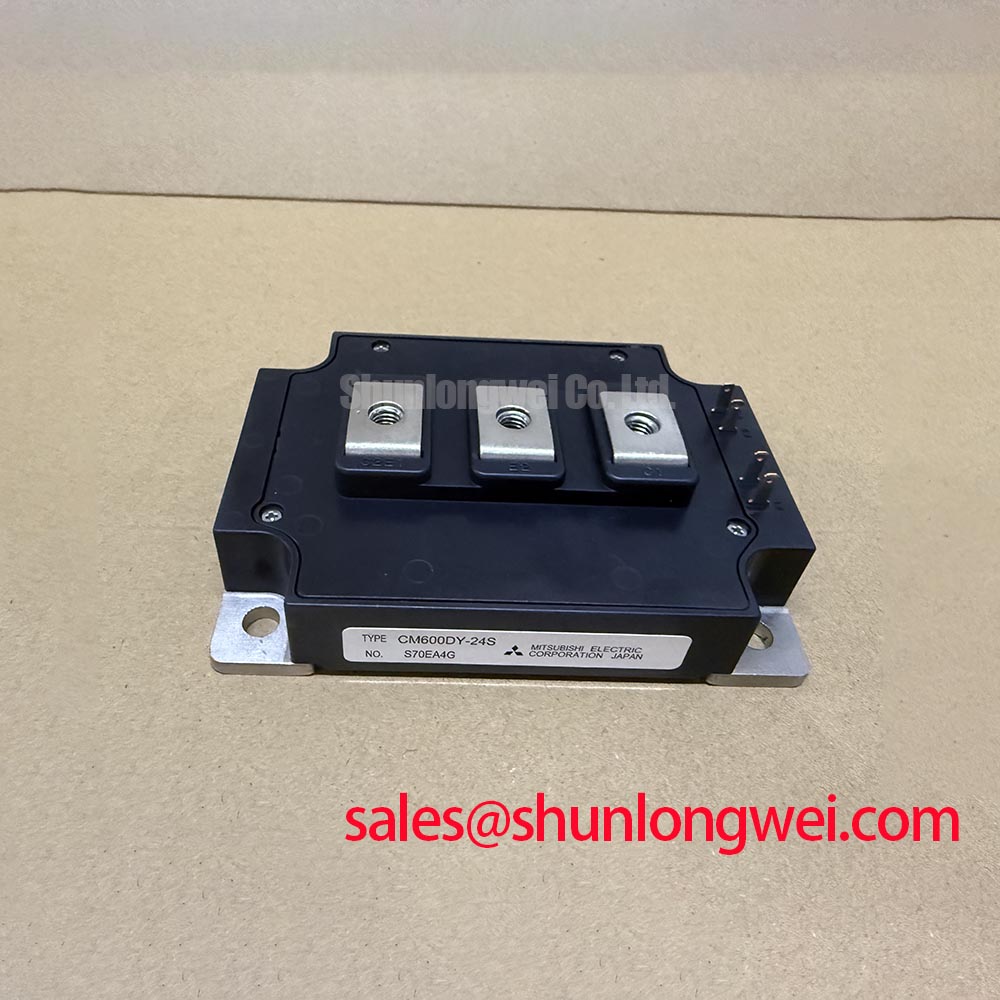
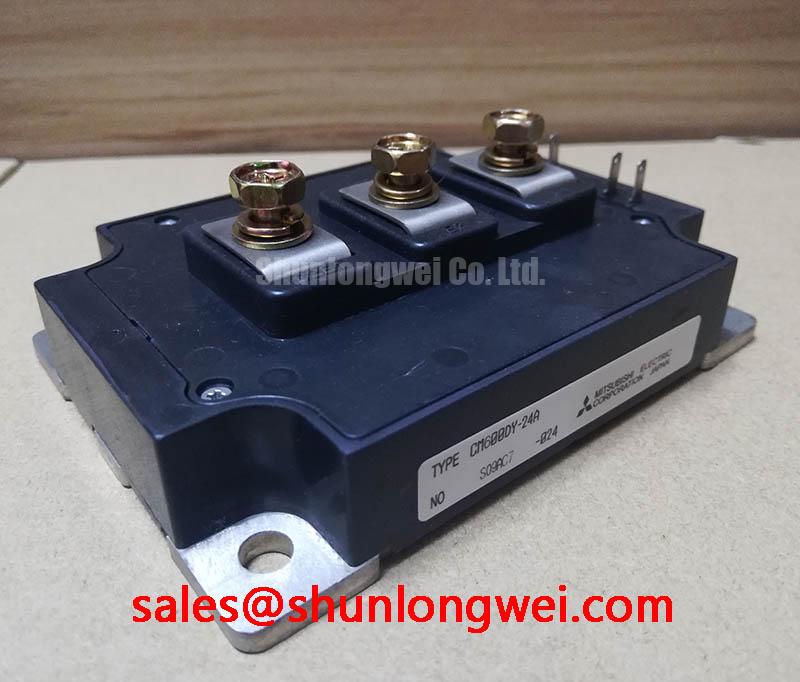
For field evaluation, the CM600DY-34H is a Mitsubishi Electric IGBT module specified for high power switching applications where voltage stress, current distribution, thermal transfer, and gate loop behavior must be assessed together. Its official maximum collector emitter voltage is 1700 V, while the continuous collector current is 600 A at TC = 25°C. The module also includes an FWDi path with a specified forward voltage of 3.12 V typical and 3.80 V maximum at IE = 600 A and VGE = 0 V.
| Parameter | Official Specification |
|---|---|
| Manufacturer | Mitsubishi Electric |
| Module type | IGBT module with FWDi |
| Collector emitter voltage, VCES | 1700 V |
| Continuous collector current, IC | 600 A at TC = 25°C |
| Isolation voltage, VISO | 4000 V AC for 1 minute, main terminal to base |
| VCE(sat) | 2.75 V typical, 3.30 V maximum at IC = 600 A, VGE = 15 V, Tj = 25°C |
| FWDi forward voltage, VEC | 3.12 V typical, 3.80 V maximum at IE = 600 A, VGE = 0 V |
| Total gate charge, QG | 2.00 µC at VCC = 850 V, IC = 600 A, VGE = 15 V |
| IGBT thermal resistance, Rth(j-c)Q | 0.016 K/W per half module |
| FWDi thermal resistance, Rth(j-c)R | 0.064 K/W per half module |
Start commissioning with an isolation audit from the main terminals to the baseplate, using the equipment manufacturer’s approved insulation procedure. The terminal to baseplate insulation resistance test voltage and acceptance limits should come from that procedure. The measurement should be made with the power circuit isolated, the gate terminals protected from the tester output, and the result recorded for each relevant terminal combination.
A changing or unexpectedly low reading can justify a closer examination of the DBC ceramic substrate, contamination paths, moisture, mounting damage, or creepage surfaces. Airborne dust can become conductive when combined with humidity and switching residue, so the inspection should include the full distance between the energized terminal region and the grounded base. Do not rely on a single resistance value to identify a ceramic crack. Compare the readings between corresponding power paths, inspect for localized contamination, and repeat the test after controlled cleaning and drying where the equipment procedure permits.
The baseplate should sit evenly on a clean, mechanically stable heat spreader. Any rocking, localized gap, or uneven clamping can distort the thermal path and place mechanical stress into the substrate. Designers evaluating the module for traction inverters, braking choppers, or high power motor converters should also verify enclosure clearance, creepage, vibration exposure, and contamination class at the complete assembly level. The 4000 V AC isolation specification for one minute is an official module parameter, not a substitute for the finished inverter’s insulation coordination assessment.
For related application context, the Industrial Applications reference provides a broader view of IGBT use across demanding power conversion equipment.
Transient Dynamics and Electrical Design: Parallel Current Sharing on CM600DY-34H
Parallel operation depends on both static voltage characteristics and dynamic gate circuit symmetry. The specified VCE(sat) of 2.75 V typical and 3.30 V maximum is measured at a defined current, gate voltage, and junction temperature. In a properly controlled operating region, the positive temperature behavior of IGBT conduction voltage can support static current balancing because a warmer die tends to present a higher conduction voltage. This effect should be treated as a stabilizing tendency, not as permission to ignore layout mismatch or thermal imbalance.
Each parallel path should have closely matched power impedance, gate resistance, driver propagation behavior, and emitter return geometry. The gate driver must source and sink the required transient current for the selected switching profile, while the external gate resistance should be selected as a bench tuning component. Increasing resistance can reduce ringing and switching stress but may increase switching loss; reducing it can accelerate transitions while making parasitic inductance more visible. The correct value is determined by the measured gate voltage, collector emitter voltage, current slope, and device temperature during switching tests.
Do not join parallel gate loops at a remote common point and assume that equal schematic wiring produces equal switching. Route each gate path with the same physical discipline and keep the drive return separate from high current commutation paths. A current sharing review should include startup, steady conduction, regenerative braking, and fault interruption conditions. The FWDi forward voltage and its thermal resistance, specified at 0.064 K/W per half module, also matter when reverse current or regenerative operation transfers heat through the diode path.
A neighboring product such as CM350DU-5F may appear in comparative sourcing work, but its voltage, current, thermal, mechanical, and gate drive conditions must be evaluated independently rather than treated as a direct replacement.
Benchtop Waveform Tuning: Auxiliary Emitter Return Trace Separation
Separate the auxiliary emitter or driver return from the main high current emitter route when building the switching test fixture. The gate driver measures its control voltage relative to the emitter reference presented at the auxiliary connection. If the driver return shares a high di/dt copper path, the voltage developed across that common impedance can appear as false gate feedback and disturb the intended switching threshold.
The power commutation loop should be physically compact, while the control return should follow its own low noise path back to the driver. This separation is especially important when evaluating regenerative braking choppers and large braking resistor interfaces, where stored DC link energy can produce substantial transient current. The resistor bank, bus structure, snubber network, and module terminals form one switching system, so waveform tuning should observe the complete current path rather than the gate signal alone.
Use a differential probe arrangement suitable for the expected common mode voltage and measure gate to auxiliary emitter directly at the module connection. Compare that waveform with the gate driver output and with the collector emitter transition. Ringing that appears at the driver output but not at the module gate suggests a connection or probe reference issue; ringing that appears at the module gate should prompt review of loop inductance, return separation, gate resistance, and driver impedance.
Field Alert: De energize the DC link and verify stored energy has fallen to the approved safe state before reconnecting gate or power wiring.
During mechanical assembly, maintain consistent contact pressure across the thermal interface and avoid allowing a busbar or cable to pull the module terminals sideways. The recommended thermal compound method, fastener torque, and clamping arrangement should come from the applicable mechanical documentation and system procedure rather than from a generic module assumption.
Benchtop Waveform Tuning: Suppressing Cres Induced Gate Voltage Spikes
High dv/dt across the opposing switch can couple through capacitance and raise the off state gate voltage. In a half bridge, this transient can reduce the effective margin between the intended off state and unwanted turn on. The remedy is a coordinated gate drive design using a low impedance turn off path, appropriate gate loop placement, and an active Miller clamp where the driver architecture supports it.
A negative gate bias may be evaluated as part of the system protection strategy, but its magnitude, timing, isolation, and driver capability are system determined. It should not be introduced without checking the module’s gate insulation limits, driver supply behavior, startup sequencing, and fault response. The same applies to dead time. Excessive dead time increases diode conduction and commutation loss, while insufficient dead time can allow cross conduction during propagation delay and tail current interaction. The correct interval must be established from measured switching behavior across temperature and load conditions.
The published QG value is 2.00 µC at VCC = 850 V, IC = 600 A, and VGE = 15 V. Because gate charge varies with operating conditions and switching voltage, it should be used with the actual driver impedance and gate voltage waveform rather than converted into a fixed universal resistor value. Probe both upper and lower device gates during complementary switching, then check for simultaneous gate elevation, abnormal collector current, and overshoot at the module terminals.
For high voltage power semiconductor background, Mitsubishi Electric’s High Voltage HVIGBT Modules information is a useful manufacturer reference. It should not be interpreted as a certification of the complete traction inverter, braking system, EMC behavior, or railway installation.
When the module is evaluated for a high speed rail or heavy freight locomotive traction inverter, engineers should examine regenerative braking energy, DC link protection, high altitude insulation coordination, thermal cycling, and switching transients as separate verification tasks. Cosmic ray or single event burnout exposure may require a dedicated reliability assessment using the applicable system environment and manufacturer data; no FIT, SEB rate, or service life value should be inferred from the electrical ratings alone. The complete converter should also be checked for current sharing, isolation monitoring, gate driver fault handling, and mechanical retention under the intended operating profile.
In the upstream power path, a device such as CM400HG-66X may be assessed as part of a complementary rectifier or converter topology. Its suitability depends on the actual system voltage, current waveform, thermal arrangement, control method, and protection coordination.